Choosing the right Cement Plant Pump is not a simple purchasing decision. It affects material flow, energy use, maintenance time, and plant safety. A pump that looks suitable on paper may struggle with abrasive slurry, high temperatures, or irregular feeding conditions. Real operating experience shows that small specification errors can create costly interruptions.
The selection process should begin with the material itself. Cement plants may handle cement slurry, water, additives, dust-laden liquids, or thick mixtures with changing densities. Check particle size, viscosity, temperature, pH, and solids concentration before comparing pump models. Flow rate and discharge pressure also require careful measurement, not rough estimates. A reliable supplier should explain test data, wear-part life, seal options, and service requirements clearly. Ask for evidence.
Pump construction matters in harsh environments. Abrasion-resistant wetted parts can extend service life when the medium contains gritty solids. Mechanical seals may need special protection in dusty or chemically aggressive areas. Motor efficiency, control compatibility, and accessible inspection points can reduce operating costs over time. Do not judge quality by purchase price alone. That shortcut often fails.
This guide examines practical criteria for selecting a Cement Plant Pump, including application demands, pump types, materials, efficiency, maintenance, and supplier support. It also considers overlooked questions, such as emergency repair access and future production changes. No selection is perfect. Conditions change, and even experienced teams must review their assumptions before installation.
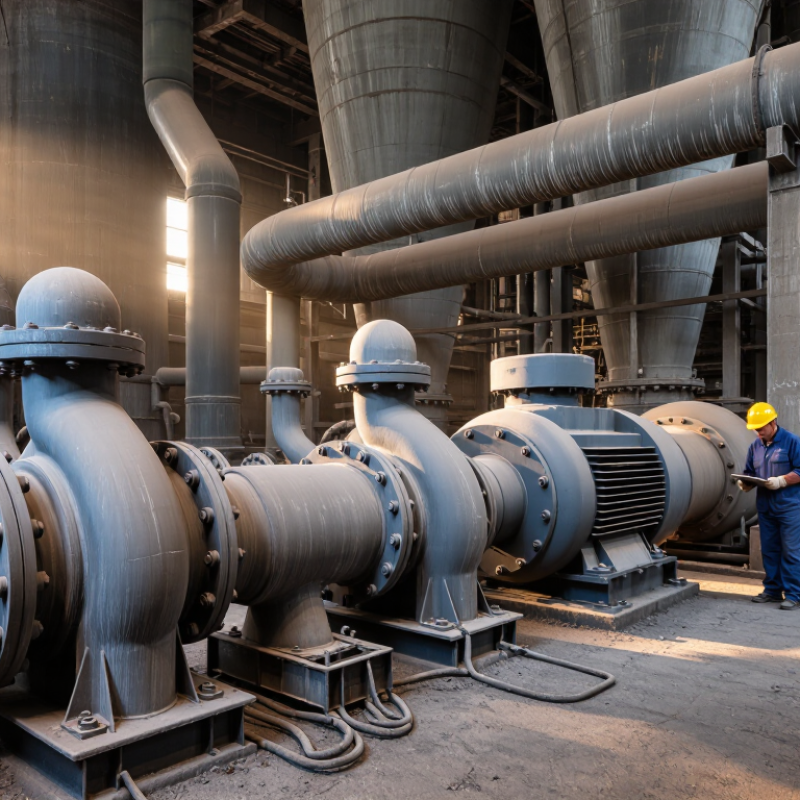
Define pump duty before comparing equipment. Cement slurry duties may range from 10 to 1,000 m³/h flow and 10 to 100 m head. Slurry density can reach 1.3 to 2.2 t/m³. These values strongly affect power, wear, and reliability. A pump moving dense material at 1,000 m³/h needs far more energy than a water pump at the same flow. Measure the actual discharge pressure, pipe length, elevation, and friction losses. Do not rely only on a catalog curve.
Tips: Record density during operation, not only in the laboratory. Check particle size and solids concentration. Allow a practical margin, but avoid excessive oversizing. An oversized pump may run inefficiently and suffer unnecessary wear.
In field inspections, impeller erosion often reveals an underestimated slurry duty. Abrasive particles can damage wet-end components, especially near bends and throttled valves. Select materials according to particle hardness, concentration, and operating temperature. Confirm that the selected pump can handle the required flow at the real system head.
For example a 200 m³/h duty at 60 m head is not interchangeable with 200 m³/h at 20 m head.
Consider seal design, maintenance access, and spare-part availability. These details matter during dusty shutdowns. A neat spreadsheet can still mislead. Actual duty may fluctuate more than expected. Recheck measurements after commissioning and adjust the operating range when necessary.
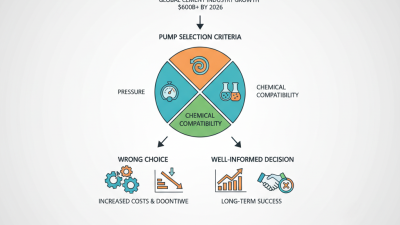
How to Choose the Right Cement Plant Pump?
In cement plants, pump selection often starts with solids concentration. Yet 30–70 wt% solids can create severe sliding abrasion. Sharp clinker dust, silica, and mineral particles attack wet-end surfaces continuously. For these duties, high-chrome alloy components are usually a practical choice. Their hardened structure resists cutting and erosion better than standard cast iron. This can extend service intervals around slurry lines, sumps, and mill discharge points.
Check more than concentration.
Particle size, shape, hardness, and slurry velocity also control wear. A pump handling coarse, angular particles needs stronger abrasion protection than one moving fine powder. High velocity may improve flow, but it can rapidly wear the impeller eye and casing throat. During inspection, look for uneven casing grooves, thinning at bends, and enlarged clearances. These details often reveal the real wear pattern.
Do not select by solids percentage alone.
A high-chrome alloy may perform poorly in highly corrosive, low-pH slurry. Temperature, chloride content, and operating hours matter too. I would also question laboratory wear data when it lacks site-specific particle information. It sounds precise, but it may mislead. Confirm the pump’s hydraulic range, shaft stability, seal arrangement, and maintainability before ordering. A slightly oversized pump can waste energy, while an undersized unit may run near its limits and wear faster. Field conditions are rarely perfect. Record actual density and flow changes before final selection.
| Cement Plant Service | Typical Material | Approx. Solids Concentration (wt%) |
Dominant Wear Mechanism | Recommended Wetted Material | Pump Configuration | Selection Rationale |
|---|---|---|---|---|---|---|
| Raw mill water spray or clean process water | Low-solids water with minor suspended fines | 0–5 | Limited abrasion; corrosion may become important depending on water chemistry | Cast iron or stainless steel, selected according to pH, chlorides, and temperature | Standard centrifugal process pump with a conventional mechanical seal | Low solids generally do not justify a heavy-duty slurry pump. Confirm corrosion resistance when the water contains chlorides or acidic contaminants. |
| Slurry transfer from limestone wet grinding | Ground limestone, water, and fine mineral particles | 15–30 | Moderate sliding abrasion and possible settling during shutdown | Natural rubber for fine, non-sharp particles; high-chrome alloy when coarse or sharp particles are present | Horizontal slurry pump with a large passage and replaceable wet-end liners | Rubber can provide good service with fine particles, while hard metal is more tolerant of coarse particles, higher temperature, and sharp mineral edges. |
| High-density limestone slurry feed | Finely ground limestone at elevated solids loading | 30–50 | Severe sliding abrasion, increased friction, and settling risk | High-chrome white iron, typically about 25–28% chromium for abrasive slurry service | Heavy-duty centrifugal slurry pump with replaceable high-chrome impeller and liners | High-chrome alloys retain hardness in abrasive service and are commonly used for dense mineral slurries. Hydraulic design must also accommodate the higher head loss. |
| Clinker cooler dust or clinker fines transport | Angular clinker particles, dust, and process water | 20–45 | High-impact and sliding abrasion; elevated temperature may be present | High-chrome alloy for severe wear; heat-resistant alloy or suitable stainless material if temperature or corrosion requires it | Heavy-duty slurry pump with temperature-compatible seals and abrasion-resistant wet-end parts | Angular clinker is more aggressive than fine limestone. Verify slurry temperature, particle size, and thermal limits before selecting elastomer liners. |
| Raw material reclaim and wash-water slurry | Clay, shale, sand, limestone fines, and water | 10–35 | Mixed abrasion with variable particle size and possible settling | High-chrome alloy for sand-rich or coarse feeds; rubber may suit predominantly fine, low-impact solids | Slurry pump with replaceable liners and an impeller designed for solids passage | Material selection should follow the hardest and coarsest fraction, not only the average solids content. Frequent sampling is useful when the feed changes seasonally. |
| Gypsum dewatering or filter-feed slurry | Gypsum crystals, water, and dissolved salts | 20–50 | Abrasion combined with possible chloride or sulfate corrosion | High-chrome alloy for abrasive duty; duplex or other corrosion-resistant alloy may be required when chemistry is aggressive | Slurry pump with corrosion-compatible shaft, seal, and fasteners | High chrome addresses abrasion but is not a universal corrosion solution. Analyze pH, chloride level, temperature, and dissolved salts before finalizing the alloy. |
| Coal, petcoke, or alternative-fuel fines slurry | Carbonaceous fines mixed with water and mineral ash | 15–45 | Moderate to severe abrasion; potential plugging or settling at low velocity | High-chrome alloy for mineral-rich feeds; rubber can be considered for fine, low-impact particles where temperature is controlled | Solids-handling slurry pump with anti-settling suction and discharge arrangement | Particle hardness and ash content strongly influence wear. Maintain adequate pipeline velocity without exceeding the pump's allowable speed or pressure. |
| Dense cement kiln dust or raw meal slurry | Fine cementitious or raw-meal particles with process water | 30–70 | Severe sliding abrasion, high viscosity, and settling tendency | High-chrome alloy wet-end parts; confirm corrosion and temperature compatibility separately | High-head, heavy-duty slurry pump with enlarged passages and replaceable liners | For 30–70 wt% solids, high-chrome alloys are a practical starting point for abrasive mineral service. Pump sizing must include slurry density, viscosity, and derated hydraulic performance. |
| Flotation or chemical-treatment slurry | Fine mineral solids with reagents, salts, or adjusted-pH water | 10–40 | Fine-particle abrasion plus chemical corrosion or elastomer attack | Material must be selected from a corrosion and compatibility review; high chrome may be suitable for abrasion but may not suit every chemical environment | Slurry pump with chemically compatible elastomers, seals, and metal parts | Solids percentage alone is insufficient. Check reagent composition, pH, temperature, chloride concentration, and seal compatibility before choosing the wetted materials. |
| Settling pond or thickener underflow | Concentrated fine mineral solids with clarified or process water | 30–70 | High-density abrasion, settling, and possible torque overload during restart | High-chrome alloy for abrasive mineral solids; rubber is generally limited to suitable fine-particle and temperature conditions | High-torque slurry pump with a solids-handling impeller and controlled startup procedure | Underflow density can vary quickly. Select the pump for the maximum credible density and verify motor power, suction conditions, and restart requirements. |
Selection note: Solids concentration is reported by weight. Final material and pump sizing should also consider particle size distribution, particle hardness, slurry temperature, pH, chloride level, flow rate, total dynamic head, suction conditions, and required wear life.
In cement plants, pump selection starts with the duty point, not the pipe connection. Cooling water, seal water, and abrasive slurry require different assumptions. Record flow, static lift, pipe length, fittings, temperature, solids concentration, and operating hours. Then calculate total dynamic head under normal and upset conditions. The U.S. Department of Energy reports that motor-driven systems can represent about 68% of industrial electricity use. Small hydraulic errors can become significant annual costs.
NPSH3 deserves closer attention. According to Hydraulic Institute ANSI/HI 9.6.1, NPSH3 is based on a 3% reduction in pump head caused by cavitation. Compare NPSHA with NPSH3 under the worst suction condition, not only during commissioning.
For water at 60°C, IAPWS property data shows vapor pressure near 19.9 kPa, equal to roughly 2.0 meters of water head. That margin disappears quickly through a blocked strainer or undersized suction pipe. Keep a documented NPSH3 margin, and verify it during hot operation.
Specify hydraulic efficiency above 70% near the preferred operating region, rather than at one isolated point. Measure flow, suction pressure, discharge pressure, and motor power after installation. Recheck them after three months. Wear, slurry buildup, and valve changes can shift the duty point. A neat spreadsheet can still be wrong. That is uncomfortable, but field data should correct it. The DOE Pumping System Assessment Tool can help compare throttling losses, speed control, and annual energy use.
How to Choose the Right Cement Plant Pump?
Select Seals and Drives for 90–150°C Service at 1,450–1,780 rpm
Cement slurry pumps face heat, abrasion, and persistent dust. At 90–150°C, seal selection becomes a reliability decision, not a minor detail. A seal must match the slurry chemistry, pressure, shaft speed, and temperature changes. Mechanical seals usually need compatible faces, elastomers, and cooling arrangements. Confirm every material against actual process data.
The drive also deserves close attention. At 1,450–1,780 rpm, poor alignment can create vibration, heat, and premature bearing wear. Select a motor and coupling with suitable service capacity for startup loads. A variable-frequency drive can improve process control, but it may expose resonance or cooling problems. Check the operating range carefully. A pump may perform well at one speed, then struggle after a small adjustment.
Tips: Record temperature at the seal chamber, not only at the discharge line. Inspect vibration trends weekly. Keep spare seal parts protected from cement dust. Do not rely on catalogue ratings alone. Field conditions are often harsher than expected. I have seen apparently correct selections fail because flushing water was warm, dirty, or inconsistent. Leave room to question the first design. That pause can prevent an expensive shutdown.
Seal and drive selection for continuous service at 90–150°C and 1,450–1,780 rpm
The chart shows typical engineering selection envelopes. Silicon-carbide mechanical seal faces are commonly preferred for abrasive cement slurries, while elastomer compatibility must be verified against the liquid and temperature. Four-pole motors typically provide approximately 1,450 rpm at 50 Hz and 1,750–1,780 rpm at 60 Hz; final selection should confirm pump load, viscosity, solids concentration, cooling, and the actual seal manufacturer’s rating.
Cement plants punish weak pump decisions. Dust enters seals, slurry abrades impellers, and shutdowns disrupt kiln production.
Begin with ISO 5199 compliance, not only the quoted flow and head. Check materials, shaft sealing, bearing arrangements, pressure limits, inspection records, and test documentation. ISO 5199 defines technical requirements for centrifugal pumps, while ISO 9906 can support witnessed hydraulic performance testing. This distinction matters. A supplier may claim compliance without proving duty-point performance.
Lifecycle value needs a practical TCO model. Include purchase cost, motor electricity, spare parts, seal replacement, labor, downtime, and disposal. The U.S. Department of Energy reports potential pumping-system energy savings of 20–50% through proper assessment and optimization. Energy can quietly dominate costs.
In a cement plant, compare five-year or ten-year consumption using actual operating hours, not ideal catalog figures. Use measured slurry density and seasonal flow changes. Small assumptions become expensive.
Ask for test curves and tolerances. Then challenge them. Is the curve based on clear water instead of cement slurry? That weakness is common. Calculate annual energy from kW, operating hours, and local tariffs. Add a downtime scenario with a realistic repair window.
The Hydraulic Institute also emphasizes system-level pump selection, because throttling and oversized motors waste energy. A cheaper pump may be costly after eighteen months. ISO documents improve confidence, but they do not replace site experience, inspection, or honest operating data.